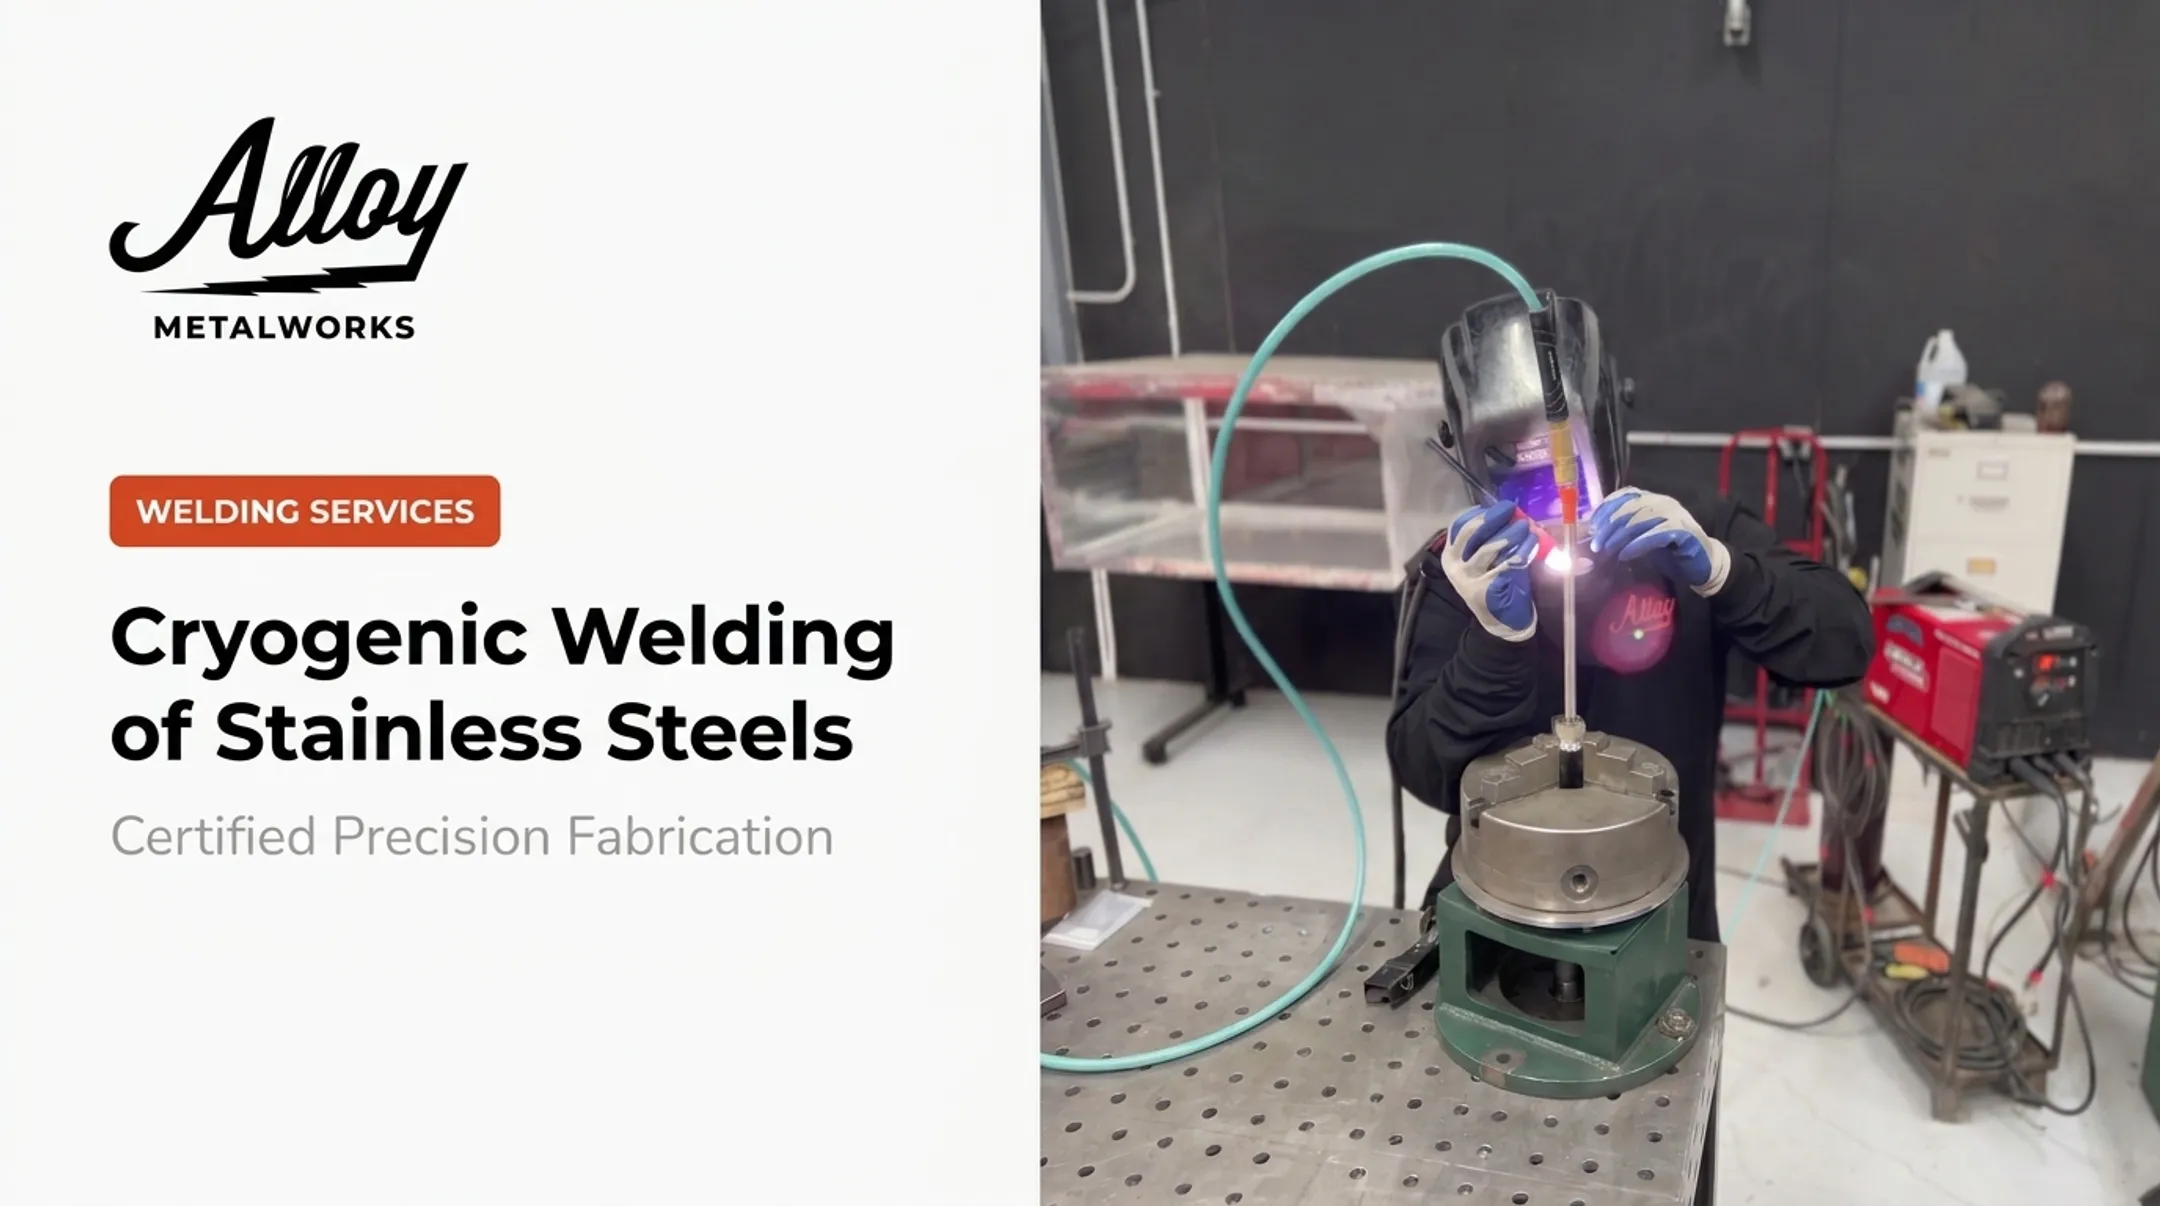
Can you weld 9% nickel steel? Yes — but only with matched nickel-based filler metals, tightly controlled heat input, and welding procedures qualified under ASME Section IX. There's no shortcut here.
This article breaks down the metallurgy, the filler metal choices, the process parameters, and what separates a qualified welding partner from one that's guessing.
Key Takeaways
- 9% nickel steel needs nickel-based fillers (12-14% Ni or ERNiCrMo-3/Alloy 625), not matching-composition consumables
- Heat input and interpass temperature control protect toughness in the heat-affected zone
- Preheat can run as low as 50°F, far below other structural steels
- Post-weld heat treatment is usually skipped unless thickness exceeds code thresholds
- ASME Section IX-qualified welders and procedures aren't optional for cryogenic vessels
What Is 9% Nickel Steel and Why It's Used in Cryogenic Applications
9% nickel steel is a low-carbon alloy steel with 8.5-9.5% nickel, minimal carbon (≤0.13%), and controlled manganese, phosphorus, and sulfur content. That nickel content stabilizes the steel's microstructure, keeping it tough instead of brittle when temperatures plunge.
Why this matters: Ordinary steel loses toughness as it cools. Cryogenic-grade steels are engineered to resist that failure mode down to -196°C, as Dillinger's technical materials confirm.
That range covers:
- LNG (methane) storage and transport
- Liquid oxygen and argon storage
- Industrial gas processing equipment
The Spec Sheet Landscape
US federal regulations recognize ASTM A353 (double normalized and tempered) and A553 (quenched and tempered) as the 9% nickel grades qualified to -320°F, roughly -196°C, per 46 CFR 54.25-20. European fabricators reference EN 10028-4.
Compared to lower-nickel alternatives, the differences are meaningful:
| Nickel Content | Approx. Service Limit |
|---|---|
| 3.5% Ni | Down to roughly -100°C |
| 5% Ni | Down to roughly -120°C to -165°C |
| 9% Ni | Down to -196°C (-320°F) |
That -196°C capability is why 9% nickel dominates LNG and industrial-gas work. US LNG exports climbed from 0.5 Bcf/d in 2016 to 15.0 Bcf/d in 2025, with export capacity expected to nearly double by 2031, according to the EIA. The result is sustained demand for 9% nickel fabrication across storage, marine, and hydrogen-adjacent infrastructure.

Key Welding Challenges With 9% Nickel Steel
Welding this alloy isn't like welding standard carbon steel. Several failure modes show up specifically in this material.
Hot cracking and grain growth. Excessive heat input causes grain coarsening in the heat-affected zone (HAZ). Contamination from sulfur, phosphorus, or lead raises this risk further and embrittles the weld area.
Filler strength mismatch. Early nickel consumables carried lower tensile strength than the base metal. Higher-strength options like ERNiCrMo-3/Alloy 625-type fillers close that gap, though TWI notes that proof strength in TIG, MIG, and SAW weld metal can still trail the base material spec — designers need to account for this.
Arc blow from residual magnetism. This is a quirk specific to 9% nickel steel. TWI identifies it as a recurring problem, mitigated through:
- Handle electrodes carefully and keep arc length short
- Switch to AC current where the process allows
- Degauss the workpiece near the weld zone before welding
Porosity risk. Nitrogen and hydrogen contamination in the weld pool cause porosity. Solid shielding gas coverage and clean base metal are non-negotiable.
Surface contamination. Prep matters more here than on mild steel. Remove oxides, degrease thoroughly, and clear surface contaminants before striking an arc to cut cracking risk downstream.

Filler Metal Selection and Welding Process Parameters
Filler choice is where most of the engineering decisions happen.
Nickel-Based Filler Options
- 12-14% Ni fillers — the traditional workhorse for 9% Ni base metal
- ERNiCrMo-3 / Alloy 625 — higher-strength option that better matches parent-metal toughness and tensile properties
Cost and strength-matching drive the trade-off. Alloy 625-type fillers cost more but close the strength gap that plagued older nickel consumables.
Preferred Processes
Process choice is driven by heat-input control:
- GTAW (TIG) and GMAW — primary processes for most 9% nickel steel fabrication
- SMAW — acceptable for certain joint configurations
- SAW — generally avoided; high heat input works against HAZ protection
Parameters That Matter
- Heat input: TWI guidance is roughly 2.5 kJ/mm for manual metal arc and up to 3.5 kJ/mm for SAW
- Interpass temperature: Keep below 150°C (302°F) where possible; TWI cites 250°C (482°F) as an upper ceiling
- Shielding gas: Pure argon, or argon with limited CO2 per the consumable data sheet (some GMAW wires specify Ar + 15–25% CO2)
Confirm heat-input limits against your qualified WPS, not generic ranges. Product-level toughness data is still useful context: Oerlikon reports SAW weld metal above 70 J / ~52 ft-lbf (ISO-V) at -196°C (-321°F) for 625-type consumables. Your governing code and WPS/PQR set the real acceptance criteria.

At Alloy Metalworks, weld procedure development locks in heat input and distortion control before the first bead, so limits are proven in the PQR instead of rediscovered after a failed impact test.
Preheat, Post-Weld Heat Treatment, and Code Requirements
Here's the counterintuitive part: 9% nickel steel wants less preheat than most alloy steels, not more.
Why so little preheat? Its high austenite content tolerates hydrogen well, substantially cutting cold-cracking risk. TWI cites ASME B31.3 examples requiring as little as 50°F (10°C) minimum preheat — a fraction of what you'd apply to comparable-thickness carbon or low-alloy steel.
PWHT is often skipped entirely. Per TWI's summary of the governing standards:
- EN 13445-4 recommends avoiding PWHT altogether for 9% Ni construction
- ASME B31.3 typically only triggers PWHT above 2 in. (51 mm) of section thickness
Always verify these figures against the current edition of your project's governing code — codes get revised, and a WPS built on outdated thresholds is a compliance gap waiting to surface during inspection.
Procedure qualification: Every WPS needs to be qualified under ASME Section IX, with welder qualification and production testing tracing back to that governing document. There's no informal version of this for pressure-retaining cryogenic equipment.
Applications and Industries Relying on 9% Nickel Steel Welding
9% nickel steel shows up wherever cryogenic liquids need reliable, long-term containment:
- LNG storage tanks — the material's original and still primary application, in service since the early 1960s
- Cryogenic pressure vessels for liquid oxygen, nitrogen, and argon
- Marine LNG fuel tanks — increasingly common as shipping shifts toward LNG propulsion
- Industrial gas processing systems — piping, cold boxes, and related process equipment
Nippon Steel's research indicates that 9% nickel steel isn't sufficient for liquid hydrogen service at 20K. It is proven for LNG and comparable cryogenic ranges, not as a universal cryogenic solution.

Those uses sit in advanced energy and cryogenic infrastructure: LNG containment, industrial gas systems, and related climate-tech buildouts where Alloy Metalworks supports precision welding on high-spec assemblies. A flawed weld in any of these systems creates catastrophic failure risk, unplanned downtime, and regulatory non-compliance that can shut a facility down.
Why Work With a Certified Welding Partner for 9% Nickel Steel
Cryogenic vessel welding isn't a place to learn on the job. Alloy Metalworks holds ASME Section IX certification and operates under ISO 9001-controlled processes, the qualification framework that governs exotic alloy welding on safety-critical equipment.
What that looks like in practice:
- Inspection-ready fabrication with full documentation and traceability, reducing downstream delays for aerospace, energy, and research clients
- Weld procedure development built around the specific material, joint configuration, and service conditions rather than a generic template
- Engineering collaboration from initial process validation through production optimization
Chris Gavitt, Alloy Metalworks' Technical Director, brings ASME Section IX and multiple AWS certifications to every project. He has worked with materials from Inconel to titanium across aerospace and energy applications. That cross-material fluency matters when a 9% nickel job includes dissimilar-metal transitions or unusual joint geometries.
For teams building cryogenic or hydrogen-adjacent infrastructure, Alloy Metalworks' energy systems fabrication starts with weld procedure qualification before fabrication begins, not after.
Frequently Asked Questions
Can you weld 9% nickel steel?
Yes. It requires nickel-based filler metals like ERNiCrMo-3, controlled heat input, and low preheat, all under ASME Section IX-qualified procedures for reliable cryogenic performance.
What filler metal is used for welding 9% nickel steel?
Nickel-based fillers with 12-14% nickel content, or Alloy 625/ERNiCrMo-3 type consumables, are standard. They match strength and toughness requirements at cryogenic temperatures.
Why does 9% nickel steel require such low preheat compared to other steels?
Its high austenite content tolerates hydrogen well, substantially reducing cold-cracking risk even at minimal preheat — as low as 50°F (10°C) in some ASME B31.3 examples.
Is post-weld heat treatment required for 9% nickel steel?
Generally no. European codes like EN 13445-4 recommend avoiding it entirely, while ASME B31.3 typically only requires it above 2 inches (51 mm) of thickness.
What causes cracking when welding 9% nickel steel?
Contamination from sulfur, phosphorus, and lead, combined with excessive heat input that causes grain growth in the heat-affected zone, are the main culprits.
What industries use 9% nickel steel the most?
LNG storage and transport, cryogenic gas processing, and marine LNG fuel tank fabrication are the primary users, with growing relevance to hydrogen infrastructure.